logo
Supal (Changzhou) Precision Tools Co.,Ltd
درباره ما
شريک حرفه اي و قابل اعتماد شما
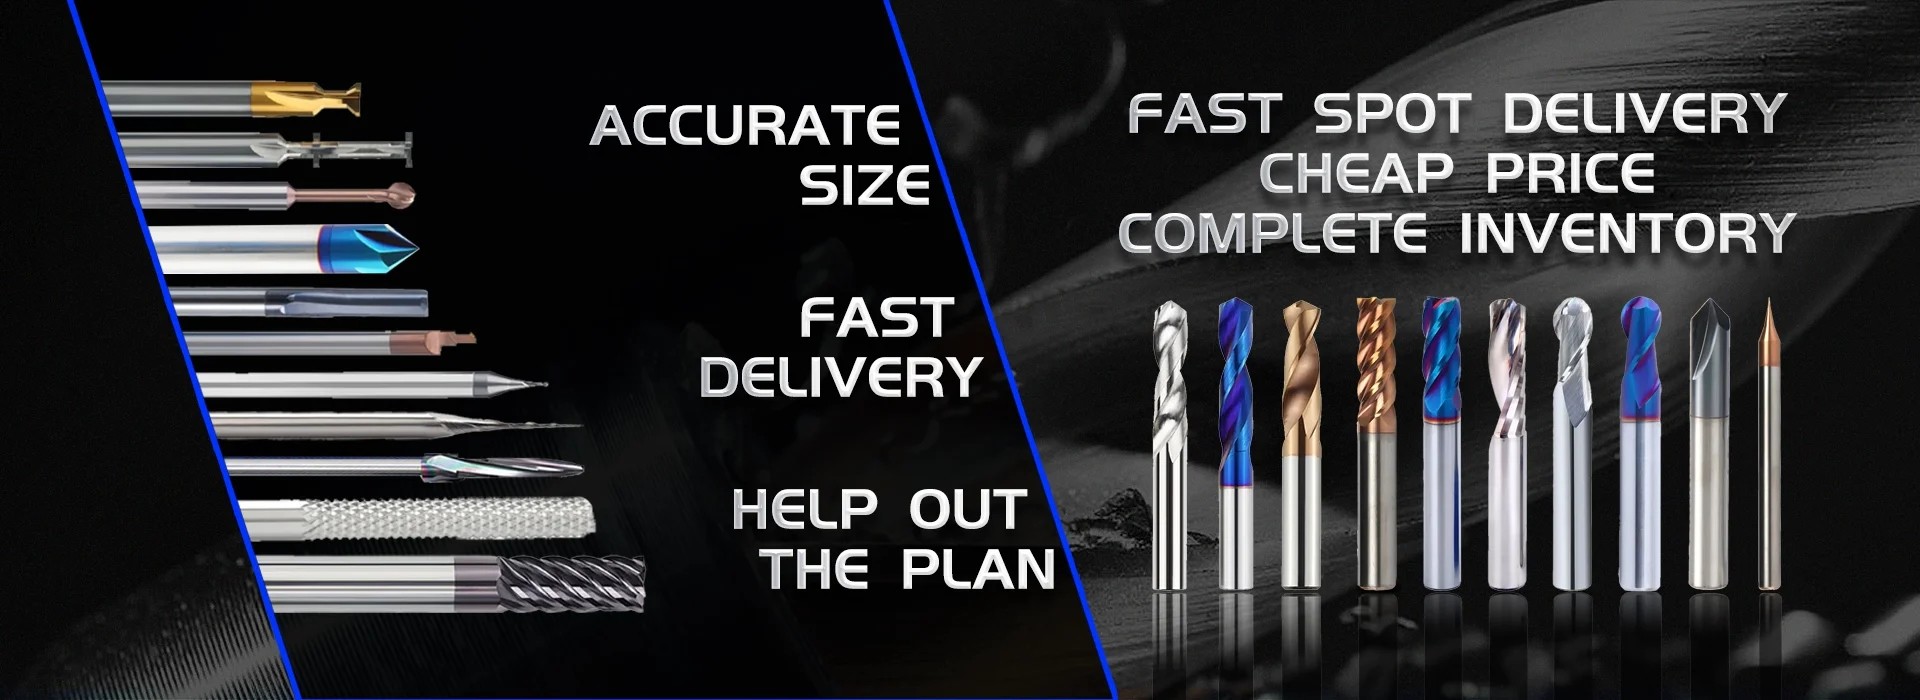
سوپال (چانگژو) ابزار دقیق Co، Ltd.برای سالهای زیادی در طراحی، تولید و بازاریابی ابزار های کربید جامد مشغول بوده است،با سرمایه گذاری کلی بیش از 10 میلیون دلار، و متشکل از یک گروه از کارمندان با تجربه است.به عنوان یک سازنده ابزار حرفه ای، آن را به یکی از اعضای مدیر انجمن ابزار چانگژو Xiaxiashu تبدیل شده است. شرکت والتر و Schutte از آلمان معرفی کرده است،ANCA از استرالیا و ماشین های تراش تراش پنج شاخه NCعلاوه بر این، این شرکت مجهز به آشکارگر خودکار ZOLLER و آشکارگر چند منظوره فوق دقیق PG1000 ...
بیشتر بدانید

0

سال تاسیس:

0

میلیون+
کارکنان

0

میلیون+
فروش سالانه:
چین Supal (Changzhou) Precision Tools Co.,Ltd کیفیت بالا
مهر اعتماد، چک اعتبار، RoSH و ارزیابی توانایی تامین کننده. شرکت دارای سیستم کنترل کیفیت و آزمایشگاه تست حرفه ای است.
چین Supal (Changzhou) Precision Tools Co.,Ltd توسعه
تیم طراحی حرفه ای داخلی و کارگاه ماشین آلات پیشرفته می تونیم با هم همکاری کنیم تا محصولاتی که شما نیاز دارید رو توسعه بدیم.
چین Supal (Changzhou) Precision Tools Co.,Ltd تولید
ماشين هاي پیشرفته اتوماتيك، سيستم کنترل سختي فرآیند ما مي تونيم تمام ترمينال هاي الکتريکي رو فراتر از نياز شما بسازيم
چین Supal (Changzhou) Precision Tools Co.,Ltd 100درصد خدمات
بسته بندی عمده و سفارشی کوچک، FOB، CIF، DDU و DDP. اجازه بدید به شما کمک کنیم تا بهترین راه حل را برای همه نگرانی هایتان پیدا کنید.

کیفیت ابزار آسیاب کربید & آسیاب های پای مربع سازنده

محصولاتی را بیابید که نیازهای شما را بهتر برآورده کنند.
پرونده ها و اخبار
آخرین نقاط داغ
Carbide Reamer Chatter and Oversize Holes: A Troubleshooting Guide
Carbide Reamer Chatter and Oversize Holes: A Troubleshooting Guide Reaming is often treated as a simple finishing operation: drill the hole, run the reamer, and expect size and surface finish to improve. In practice, carbide reaming is sensitive to allowance, alignment, rigidity, coolant delivery, edge geometry, and parameter stability. When any of these variables are wrong, the process may produce chatter marks, oversize holes, poor roundness, tapered holes, edge chipping, or unexpectedly short tool life. For CNC machinists, process engineers, and purchasing engineers, the key point is this: reamers do not correct every drilling problem. A reamer can improve a prepared hole, but it cannot reliably fix a severely misaligned, scratched, undersized, bell-mouthed, or unstable pre-hole. This guide explains how to diagnose carbide reamer chatter and hole tolerance problems step by step, so corrective action is based on the failure mode rather than guesswork. Why Reaming Problems Are Difficult to Diagnose A carbide reamer cuts with multiple teeth at once and removes only a small amount of material. Because the operation is light compared with drilling or milling, many shops assume that reaming should be forgiving. In reality, the small stock allowance and the tight tolerance target make the process less forgiving. If the reaming allowance is too small, the tool may rub instead of cut. If the allowance is too large, the cutting edges can be overloaded. If the drilled hole is not straight, the reamer may follow the existing error or be forced to cut unevenly. If the holder or fixture lacks rigidity, small vibration can appear as visible chatter lines inside the hole. This is why the same reamer may produce an excellent finish in one setup and fail in another setup with the same nominal hole diameter. Common Symptoms in Carbide Reaming Chatter Marks Inside the Hole Chatter marks usually appear as repeated spiral or polygon-like patterns on the hole wall. They indicate that the tool, holder, workpiece, or machine structure is vibrating during the cut. Chatter may be caused by excessive allowance, insufficient rigidity, poor alignment, incorrect speed, or an unstable pre-hole. Oversize Holes After Reaming An oversize hole can be caused by tool runout, misalignment, excessive cutting pressure, thermal expansion, or chips trapped between the reamer and hole wall. If oversize holes repeat consistently, measure runout and check the pre-hole condition before assuming the reamer diameter is wrong. Poor Surface Finish Poor surface finish after reaming can come from built-up edge, inadequate coolant, chip recutting, poor drill preparation, or a worn cutting edge. When a reamer is forced to remove uneven stock, the surface finish often becomes worse even if the tool is sharp. Short or Inconsistent Tool Life If one reamer lasts much longer than another in the same application, review machine setup, hole preparation, coolant delivery, and part material variation. Tool coating and carbide grade matter, but process instability is often the first thing to eliminate. Edge Chipping Edge chipping on a carbide reamer often indicates impact, interrupted cutting, excessive allowance, poor entry, or hard inclusions in the workpiece. Reamers are finishing tools; they are not designed to correct large drilling errors or remove heavy stock. Root Cause 1: Incorrect Reaming Allowance The pre-hole allowance is one of the most important variables in reaming. Too little stock can cause rubbing, heat, and poor finish. Too much stock can overload the cutting edge and cause chatter or chipping. There is no universal allowance that fits every diameter, material, and reamer design. As a starting principle, small-diameter holes generally need smaller allowances, while larger holes can tolerate more stock removal. However, the correct value depends on the workpiece material, hole depth, tool geometry, coolant method, and tolerance target. Always validate allowance on the actual machine and fixture rather than copying a value from another operation. When troubleshooting, compare the actual drilled hole diameter before reaming with the final target. If the pre-hole size varies from part to part, the reaming result will also vary. Root Cause 2: Poor Pre-Hole Quality A reamer needs a stable guide. If the drilled hole is already out of position, tapered, scratched, or heavily work-hardened, reaming becomes much more difficult. Before blaming the reamer, inspect the drilling process. Check whether the drill is producing a round and straight hole, whether chips are scratching the wall, and whether the drill is walking at entry. For holemaking process control, Carbide Drills and reamers should be selected as a system, not as unrelated tools. If the drill leaves severe chip scratches or inconsistent hole size, the reamer may not have enough control to repair the defect. Improve drilling stability first, then evaluate the reaming pass. Root Cause 3: Runout and Misalignment Runout is one of the fastest ways to produce oversize holes and uneven tool wear. A small amount of runout at the holder or spindle can make one cutting edge do more work than the others. This creates uneven cutting pressure, poor roundness, and shorter tool life. Check runout at the tool shank and near the cutting section when possible. Also review holder condition, collet cleanliness, spindle condition, and whether the tool is clamped with enough contact length. For precision holes, the toolholding system is as important as the reamer itself. Misalignment can also occur when the reamer enters a hole that is not coaxial with the spindle path. This is common when previous operations, fixtures, or long-reach setups introduce deflection. Root Cause 4: Speed, Feed, and Cutting Stability Reaming parameters should be stable enough to cut cleanly without rubbing or vibration. Too high a speed can increase heat and worsen chatter in some materials. Too low a feed can cause rubbing rather than cutting. Too high a feed can overload the edge and damage surface finish. For troubleshooting, adjust one variable at a time. If chatter appears, reducing speed slightly may help, but only if rigidity and allowance are already reasonable. If the tool rubs and produces heat, increasing feed within a safe range may sometimes improve cutting action. Parameter changes should be verified through trial cuts on the actual part material. Avoid using generic speed and feed tables as final values. Treat them as starting references and adjust based on hole size, depth, machine rigidity, coolant, and tolerance requirements. Root Cause 5: Coolant and Chip Control Although reaming removes less material than drilling, chips still matter. Fine chips or particles trapped inside the hole can scratch the wall and damage the cutting edges. Coolant helps flush chips, reduce heat, and stabilize the cutting zone. For blind holes, chip evacuation becomes more difficult because chips have limited space to leave the bottom of the hole. Coolant direction, pressure, and flow should be reviewed carefully. If chips remain in the hole from drilling, clean or flush the hole before reaming. Coolant concentration and filtration also matter. Contaminated coolant can carry abrasive particles back into the hole, affecting surface finish and tool life. Root Cause 6: Reamer Geometry and Application Fit Different Carbide Reamers are designed for different applications. Factors such as flute design, lead angle, margin design, edge preparation, and coating can influence cutting stability and chip evacuation. A reamer for through holes may not behave the same way in blind holes. A reamer optimized for aluminum may not be ideal for stainless steel or hardened material. A long reamer may require extra attention to rigidity and runout. When discussing a reamer problem with a supplier, provide the workpiece material, pre-hole diameter, target tolerance, hole depth, through-hole or blind-hole condition, coolant method, current parameters, and photos of the hole surface if available. This information helps determine whether the solution is a geometry change, parameter change, or process correction. A Practical Troubleshooting Workflow Step 1: Measure the Pre-Hole Before checking the finished hole, measure the drilled or bored hole before reaming. Record diameter, roundness, straightness if possible, and surface condition. If the pre-hole is unstable, fix it first. Step 2: Check Tool Runout Measure runout in the actual holder. Clean the shank, collet, and holder. Replace damaged holders or worn collets. If runout is reduced and oversize holes improve, the reamer was not the primary cause. Step 3: Review Allowance Compare actual pre-hole diameter with the reamer size. If allowance varies between parts, identify why the drilling or boring operation is inconsistent. Step 4: Inspect Chips and Surface Finish Look for chips trapped in the hole, scratches, or rubbing marks. If chip scratches appear, improve coolant flushing and pre-hole cleaning. Step 5: Adjust Parameters Gradually Change speed, feed, or coolant one factor at a time. Record results. Avoid changing tool geometry and parameters simultaneously unless the current setup is clearly unsuitable. Step 6: Review Tool Selection If the process is stable but the problem remains, review reamer geometry, coating, flute style, and edge preparation. For related machining and finishing applications, Supal also provides Carbide Milling Tools for broader CNC process planning. Common Mistakes to Avoid Mistake 1: Expecting the Reamer to Fix a Bad Hole A reamer is a finishing tool, not a rescue tool. If the drilled hole is severely off-center, tapered, or scratched, improve the pre-hole first. Mistake 2: Ignoring Runout Runout can make an accurate reamer cut oversize. Always measure the tool in the actual holder instead of assuming the tool itself is incorrect. Mistake 3: Using Too Little Allowance Too little material can cause rubbing, heat, and poor finish. The tool must cut, not polish irregular stock. Mistake 4: Using Too Much Allowance Too much material can overload the cutting edges and cause chatter, chipping, or poor roundness. Mistake 5: Changing Reamer Diameter Before Checking the Process If the hole is oversize because of runout, misalignment, or chatter, changing tool diameter may not solve the root problem. FAQ Why does my carbide reamer produce an oversize hole? Common causes include runout, misalignment, excessive allowance, unstable pre-hole quality, trapped chips, or thermal effects. Measure runout and pre-hole size before assuming the reamer diameter is incorrect. Can a reamer correct drill wander? Only to a limited degree. If the drilled hole is significantly off-position or not straight, the reamer may follow the existing error. Improve the drilling or boring process first. What causes chatter during reaming? Chatter can result from excessive allowance, poor rigidity, incorrect speed, long tool overhang, unstable pre-hole geometry, or poor alignment between spindle and hole. Should I reduce speed or feed to stop reamer chatter? Sometimes reducing speed helps, but it is not always the first solution. Check runout, allowance, holder rigidity, and pre-hole quality first. Feed that is too low can also cause rubbing. What information should I send when asking for reamer troubleshooting support? Send the workpiece material, pre-hole diameter, target diameter and tolerance, hole depth, through-hole or blind-hole condition, coolant method, current speed/feed, tool overhang, holder type, and photos of the hole surface or worn reamer. Conclusion Carbide reamer chatter, oversize holes, and short tool life are usually process problems, not just tool problems. The most effective troubleshooting sequence is to measure the pre-hole, check runout, review allowance, inspect surface marks, and adjust parameters one variable at a time. If you are facing unstable hole tolerance, chatter marks, or short reamer life, Contact Supal with your workpiece material, pre-hole condition, target tolerance, current parameters, and failure photos. Supal can help evaluate whether the root cause is allowance, runout, coolant, reamer geometry, or overall process stability.
2026

09/29

Carbide Drill Chip Evacuation: How to Prevent Chip Packing and Breakage
Carbide Drill Chip Evacuation: How to Prevent Chip Packing and Breakage Chip evacuation is one of the most important conditions for stable carbide drilling, especially in deep holes, blind holes, stainless steel, alloy steel, aluminum, and other materials where chips can curl, compress, or weld inside the flute. A carbide drill may have the correct diameter, coating, and carbide grade, but if chips cannot leave the hole smoothly, cutting load rises rapidly. The result may be poor hole finish, oversized or tapered holes, edge chipping, sudden drill breakage, or a workpiece scrap problem that is much more expensive than the tool itself. For CNC machinists, process engineers, and purchasing teams, chip evacuation should not be treated as a minor detail after tool selection. It is part of the drilling process design. The correct solution is usually a combination of drill geometry, coolant strategy, pecking method, entry stability, and conservative parameter validation. This guide explains how to diagnose chip packing in carbide drilling and how to adjust the process without guessing. Why Chip Evacuation Matters in Carbide Drilling Unlike milling, where chips often have open space to leave the cutting zone, drilling traps the cutting edges inside a narrow hole. The chip must form, curl, travel along the flute, and leave the hole before it is re-cut or compressed. When the chip path becomes restricted, several failure mechanisms can appear at the same time: Chips jam between the drill flute and hole wall, increasing torque. Re-cut chips damage the cutting edge and leave scratches inside the hole. Heat accumulates because chips carry heat out of the cutting zone less effectively. Coolant cannot reach the cutting edge, especially in blind or deep holes. The drill body may deflect or seize, causing catastrophic breakage. This is why two drills with similar material and coating can perform very differently in the same hole depth. The one with better chip control and coolant access may deliver more stable results even if its catalog specifications look similar. Common Symptoms of Poor Chip Evacuation Sudden Torque Increase A gradual increase in spindle load or a sudden torque spike during drilling often indicates that chips are no longer leaving the hole smoothly. If the problem appears after the drill reaches a certain depth, chip packing is more likely than simple edge wear. Broken Drill Near the Flute or Shank Transition When chips jam in the hole, the drill may stop rotating freely while the machine continues to feed. This can create high torsional stress and break the drill. If breakage happens repeatedly at similar depths, review chip evacuation before changing only the carbide grade. Scratched or Rough Hole Wall Long, tangled, or re-cut chips can rub against the hole wall and damage the surface. In precision holes, this can also affect the later performance of Carbide Reamers, because reaming cannot fully correct severe drilling damage or poor hole straightness. Built-Up Edge on the Drill Margin In aluminum and some stainless steels, poor evacuation can combine with adhesion. Chips may weld to the cutting edge or margin, increasing friction and making the drill cut unevenly. Inconsistent Hole Size or Location If chips are trapped unevenly on one side of the drill, the tool can be pushed off center. This may cause oversized holes, poor roundness, or positional error even when the tool itself is not visibly worn. Main Causes of Chip Packing Flute Geometry Not Matched to Chip Volume Drills with insufficient flute space may perform acceptably in shallow holes but struggle as depth increases. A material that forms long or thick chips needs enough flute volume to carry those chips out. When flute space is limited, chips compress inside the hole. For difficult applications, the selection of Carbide Drills should consider not only diameter and coating, but also flute form, helix, margin design, and coolant hole availability. Feed and Speed Do Not Produce Manageable Chips Chip thickness is controlled largely by feed per revolution. If the feed is too low, chips may become thin, stringy, and difficult to break. If the feed is too high, chips may become thick and overload the flute. Cutting speed also affects heat and material behavior. The goal is not simply to reduce feed whenever drilling becomes unstable. In some materials, slightly increasing feed within a safe range can improve chip breaking. However, any adjustment should be validated gradually on the actual machine, fixture, and workpiece material. Coolant Cannot Reach the Cutting Edge Coolant does more than reduce temperature. It also helps push chips out of the hole. External coolant may be enough for shallow drilling, but it often becomes less effective as hole depth increases. Through-coolant drills can improve chip evacuation in many deep-hole applications, provided coolant pressure, flow, and filtration are adequate. If coolant pressure is weak, chips may remain in the flute even with a through-coolant tool. If the coolant hole is blocked by fine chips or contamination, the process may fail suddenly after earlier stable operation. Blind Hole Bottom Effects Blind holes create a special challenge because chips cannot pass through the workpiece. Chips collect near the bottom, and as the drill approaches final depth, there is less space for chip movement. This can cause a torque spike at the end of the hole. For blind holes, process engineers should pay special attention to final-depth feed strategy, chip clearing cycles, and whether the required flatness or bottom condition is realistic with the chosen tool. Incorrect Pecking Strategy Peck drilling can help clear chips, but excessive pecking can also reduce efficiency and may cause rubbing if the tool repeatedly re-enters poorly. Too little pecking can leave chips packed in the flute. A suitable peck strategy depends on material, hole depth, coolant, drill diameter, and machine rigidity. As a starting reference, deeper holes and poor chip-breaking materials usually require more controlled chip clearing, while stable through-coolant setups may allow longer uninterrupted drilling. Exact peck depth should be validated under the actual machining conditions rather than copied from another shop. A Practical Troubleshooting Sequence 1. Identify the Depth Where Failure Begins Record whether chip evacuation issues start immediately, at mid-depth, or near final depth. If the process is stable at shallow depth but fails deeper in the hole, chip evacuation or coolant delivery is likely involved. 2. Inspect Chip Shape Look at the chips removed from the machine. Short, consistent chips are generally easier to evacuate than long stringers or compacted nests. If chips are long and tangled, adjust feed, drill geometry, or pecking strategy. If chips are powdery or overheated, review cutting speed, coolant, and edge condition. 3. Check Coolant Delivery Confirm whether coolant actually reaches the drill point. For through-coolant tools, check pressure, flow, filtration, and whether coolant holes are blocked. For external coolant, confirm nozzle direction and whether coolant still reaches the hole as depth increases. 4. Review Entry Stability Unstable entry can cause the drill to wander, generating uneven chips and side load. Spotting, center drilling, or using a suitable entry method may improve stability when the workpiece surface is angled, rough, or interrupted. For broader holemaking process planning, carbide drills should be coordinated with other Carbide Milling Tools and finishing tools rather than selected as an isolated item. 5. Adjust Parameters One Variable at a Time Avoid changing speed, feed, peck depth, coolant, and tool design all at once. Change one variable, document the result, then proceed. This makes it easier to identify the real cause of the improvement or failure. Parameter Adjustment Logic The following guidance should be treated as a starting framework, not a universal parameter table: If chips are long and stringy, review feed per revolution and drill geometry for chip breaking. If chips are blue, powdery, or heat-damaged, reduce thermal load by reviewing cutting speed, coolant, or coating choice. If chips pack at a repeatable depth, improve chip clearing at that depth through peck adjustment, coolant improvement, or drill geometry change. If the drill breaks at entry, review spot drilling, surface condition, runout, and fixture rigidity. If hole finish is poor after drilling, correct chip evacuation before relying on a reaming pass to hide the problem. For high-volume production, record load curve, chip form, tool wear, hole tolerance, and surface finish together. Tool life alone does not explain whether the root cause is chip packing, coating mismatch, poor geometry, or insufficient coolant. Common Mistakes to Avoid Mistake 1: Reducing Feed Without Checking Chip Shape Reducing feed can sometimes make chips thinner and more stringy, making evacuation worse. Always inspect chip shape before deciding whether to reduce or increase feed. Mistake 2: Using the Same Drill for Every Hole Depth A drill that works in a shallow hole may not be suitable for a deeper blind hole in the same material. Hole depth changes chip evacuation requirements. Mistake 3: Ignoring Coolant Flow A through-coolant drill does not guarantee good chip evacuation if pressure is insufficient or the coolant path is blocked. Mistake 4: Expecting Reaming to Fix Poor Drilling Reaming improves size and finish only when the pre-drilled hole is reasonably stable. Severe chip scratches, wander, or poor straightness can reduce reamer performance. Mistake 5: Changing Tool Grade Before Diagnosing Process Conditions If the drill breaks because chips are packed in the hole, switching to a tougher carbide grade may not solve the root cause. Geometry, coolant, and peck strategy should be reviewed first. FAQ What is chip packing in drilling? Chip packing occurs when chips cannot leave the hole smoothly and become compressed inside the flute or between the drill and hole wall. It increases torque, heat, and breakage risk. Is peck drilling always necessary for carbide drills? No. Some through-coolant carbide drills can drill continuously under stable conditions. Pecking is useful when chip evacuation is difficult, but excessive pecking can reduce efficiency and may introduce rubbing. The correct strategy depends on material, hole depth, coolant, and machine rigidity. Why does my drill break only near the bottom of a blind hole? Near the bottom of a blind hole, chips have less space to move and coolant flow may be less effective. Chip packing and torque spikes are common at final depth if the process is not designed for blind-hole evacuation. Can coolant pressure solve all chip evacuation problems? Coolant pressure helps, but it is not the only factor. Drill flute design, chip form, feed per revolution, pecking strategy, and hole depth also affect evacuation. Should I use a reamer after a poorly drilled hole? A reamer can improve size and finish only if the drilled hole is already reasonably stable. If the drill leaves heavy scratches or wanders because of chip packing, fix the drilling process first. Conclusion Carbide drill chip evacuation is not just a coolant issue or a feed-rate issue. It is a combined result of flute geometry, chip formation, coolant delivery, entry stability, hole depth, and process validation. When chip packing appears, the most effective response is to diagnose the failure mode step by step rather than changing tools at random. If you are facing carbide drill breakage, blind-hole chip packing, or unstable hole quality, Contact Supal with your workpiece material, hole diameter, depth, coolant condition, current drill type, and failure photos. Supal can help evaluate whether the issue is mainly related to drill geometry, coating, coolant delivery, or parameter strategy.

2026

09/24

انتخاب پوشش کاربید ابزار: PVD، DLC و پوشش های نانو مقایسه شده است
انتخاب پوشش ابزار کاربید: پوشش‌های PVD، DLC و نانو در مقایسه با یکدیگر انتخاب پوشش یکی از تصمیماتی است که اغلب حدس زده می شود در ابزار کاربید و یکی از مهم ترین آنها. عدم تطابق پوشش با مواد قطعه کار می تواند عمر ابزار را کوتاه کند، لبه ساخته شده را افزایش دهد یا هزینه را بدون سود قابل اندازه گیری افزایش دهد. با این حال، بسیاری از مغازه‌ها به جای پوششی که برای مواد و عملکرد خاص مناسب است، از هر پوششی که بیشتر آشنا است استفاده می‌کنند. این راهنما به ماشین‌کاران CNC، مهندسان فرآیند و تیم‌های خرید، روشی ساختاریافته برای ارزیابی پوشش‌های PVD، DLC و نانو ارائه می‌دهد، بنابراین انتخاب پوشش به یک تصمیم عمدی مرتبط با حالت شکستی که شما سعی در جلوگیری از آن دارید، تبدیل می‌شود، نه یک عادت پیش‌فرض. چرا انتخاب پوشش یک سایز مناسب برای همه نیست؟ یک پوشش، شیمی سطح و رفتار اصطکاک لبه برش را تغییر می دهد، نه درجه کاربید یا هندسه زیرین آن. این بدان معنی است که یک پوشش می تواند عملکرد یک ماده را بهبود بخشد و در ماده دیگر مزایای کمی یا حتی منفی داشته باشد. پوشش ها به طور کلی به یک یا چند مکانیسم زیر پاسخ می دهند: مقاومت در برابر اکسیداسیون و حرارتدر دماهای برش بالا، مربوط به فولادهای سخت شده و آلیاژهای با دمای بالا. کاهش اصطکاک و چسبندگیمربوط به مواد مستعد لبه های ساخته شده مانند آلومینیوم و برخی فولادهای ضد زنگ. مقاومت در برابر سایش، مربوط به مواد کامپوزیت و برخی از چدن ها است. روانکاری برای برش خشک یا تقریباً خشکمربوط به عملیاتی است که از خنک کننده سیل جلوگیری می کند. از آنجا که این مکانیسم ها متفاوت هستند، پوششی که برای مقاومت در برابر اکسیداسیون در فولاد سخت شده انتخاب می شود، به طور خودکار به کاهش چسبندگی در آلومینیوم ترجمه نمی شود، و برعکس نیز صادق است. پوشش های PVD: TiN، TiAlN و خانواده های مرتبط پوشش‌های رسوب بخار فیزیکی (PVD) از رایج‌ترین پوشش‌ها در ابزار کاربید هستند و خانواده وسیعی از شیمی را پوشش می‌دهند. قلع (نیترید تیتانیوم)یک پوشش همه منظوره است که سختی متوسط ​​و مقاومت در برابر اکسیداسیون را فراهم می کند. اغلب به‌عنوان یک پایه اقتصادی برای ماشین‌کاری عمومی فولاد و چدن استفاده می‌شود تا به‌عنوان راه‌حلی تخصصی برای مواد سخت‌گیر. TiAlN (نیترید آلومینیوم تیتانیوم)و انواع حاوی آلومینیوم مربوطه مقاومت اکسیداسیون بالاتری را در دماهای بالا در مقایسه با TiN ارائه می دهند، به همین دلیل است که این خانواده معمولاً با فولاد سخت شده، فولاد ابزار و برخی از کاربردهای آلیاژی با دمای بالا همراه است. محتوای آلومینیوم باعث ایجاد یک لایه اکسید محافظ در دمای منطقه برش می شود که به حفظ یکپارچگی لبه در طول برش پایدار کمک می کند. پوشش‌های PVD معمولاً در دماهای رسوب متوسط ​​اعمال می‌شوند و می‌توانند لایه‌بندی شوند یا با عناصر دیگر ترکیب شوند تا سختی، مقاومت در برابر اکسیداسیون و ویژگی‌های اصطکاک را تنظیم کنند. ساختار دقیق چند لایه و ترکیب مورد استفاده برای یک ابزار معین باید با تامین کننده تایید شود نه اینکه از یک برچسب عمومی "PVD" فرض شود، زیرا فرمولاسیون بین تولید کنندگان متفاوت است. پوشش های DLC: اصطکاک کم برای مواد مستعد چسبندگی پوشش های کربن مانند الماس (DLC) در درجه اول به دلیل اصطکاک بسیار کم و مقاومت قوی در برابر چسبندگی مواد ارزش گذاری می شوند. این امر DLC را به انتخابی متداول برای آلومینیوم، فلزات غیرآهنی و سایر مواد تبدیل می‌کند که لبه‌های ساخته شده به جای سایش حرارتی یا سایشی، حالت شکست غالب است. پوشش‌های DLC معمولاً برای برش‌های آهنی در دمای بالا توصیه نمی‌شوند، زیرا مزیت عملکردی آنها به مقاومت در برابر اصطکاک و چسبندگی کم نسبت به مقاومت در برابر اکسیداسیون در دمای بالا مرتبط است. استفاده از یک ابزار پوشش داده شده با DLC در برنامه ای که به جای چسبندگی تحت تأثیر بار حرارتی قرار دارد، ممکن است سود مورد انتظار را به همراه نداشته باشد. از آنجایی که پوشش‌های DLC در دماهای رسوب‌گذاری نسبتاً پایین در بیشتر فرآیندها اعمال می‌شوند، اغلب با لبه‌های تیز و دقیق بدون وضوح لبه‌ها سازگار هستند، که بخشی از این موضوع است که چرا DLC اغلب با ابزارهای مخصوص آلومینیوم و ریزکاری مرتبط است. پوشش های نانو و نانوساختارهای چند لایه "پوشش نانو" یک اصطلاح بازاریابی گسترده ای است که می تواند به چندین فناوری زیربنایی مختلف از جمله ساختارهای نانوکامپوزیت، پوشش های PVD نانولایه یا پوشش هایی با پالایش دانه در مقیاس نانو اشاره کند. به جای تلقی نانو به عنوان یک شیمی پوشش متمایز، دقیق تر است که آن را به عنوان یک رویکرد ساختاری در نظر بگیریم که می تواند در PVD یا سایر خانواده های پوشش برای بهبود سختی، چقرمگی یا پرداخت سطح در مقیاسی ظریف تر از پوشش های معمولی اعمال شود. هنگامی که یک تامین کننده یک پوشش را به عنوان "نانو" توصیف می کند، بپرسید که از چه شیمی پایه استفاده می کند (به عنوان مثال، یک نانوساختار TiAlN) و چه ویژگی خاصی را در نظر گرفته شده است که نانوساختار بهبود بخشد - سختی، چقرمگی، صافی سطح، یا مقاومت حرارتی - به جای اینکه "نانو" را به تنهایی به عنوان تضمین عملکرد برتر در همه مواد در نظر بگیرید. تطبیق پوشش با مواد قطعه کار پیوندهای اولیه زیر، رویه رایج صنعت هستند، نتایج تضمین شده نیستند، و باید بر اساس ابزار دقیق، فرمول پوشش، و شرایط ماشینکاری تایید شوند: آلومینیوم و فلزات غیر آهنی:پوشش‌های با اصطکاک کم و مقاوم در برابر چسبندگی مانند DLC معمولاً مورد استفاده قرار می‌گیرند زیرا لبه ساخته شده خطر اصلی است. کاربید بدون پوشش و صیقلی نیز در مواردی رایج است که کاهش اصطکاک از پرداخت سطح کافی است. فولاد ضد زنگ:معمولاً از پوشش‌هایی استفاده می‌شود که سختی متوسط ​​را با تمایلات چسبندگی کاهش می‌دهد، زیرا فولاد ضد زنگ می‌تواند هم سخت شود و هم به لبه برش بچسبد. خانواده صحیح باید بر اساس درجه و عملکرد ضد زنگ خاص تأیید شود. فولاد سخت شده و ابزار:پوشش‌هایی با مقاومت اکسیداسیون و حرارتی بالاتر، مانند پوشش‌های PVD خانواده TiAlN، معمولاً به دلیل دمای بالای منطقه برش با این مواد مرتبط هستند. تیتانیوم و آلیاژهای با دمای بالا:انتخاب پوشش در اینجا به رفتار حرارتی و واکنش شیمیایی با قطعه کار بسیار حساس است. توصیه های اختصاصی تامین کننده باید به جای اینکه از رویه عمومی پوشش فولادی فرض شود، درخواست شود. کامپوزیت ها و غیر فلزات ساینده:مزیت پوشش به شدت به محتوای فیبر و سایندگی بستگی دارد. برخی از کاربردهای کامپوزیت با ابزارهای بدون پوشش، صیقلی و لبه تیز به جای پوشش سخت، عملکرد بهتری دارند، به خصوص در مواردی که چسبندگی دغدغه اصلی نیست. چارچوبی عملی برای تصمیمات پوشش ابتدا حالت شکست غالب را شناسایی کنید قبل از انتخاب یک پوشش، تعیین کنید که آیا حالت شکست واقعی ابزار چسبندگی و لبه ساخته شده، نرم شدن حرارتی، سایش ساینده یا ترکیبی است. پوششی که برای رسیدگی به حالت خرابی اشتباه انتخاب می‌شود، ممکن است بدون حل مشکل اساسی، هزینه اضافه کند. پوشش را به عنوان یک متغیر در میان چندین متغیر در نظر بگیرید پوشش با درجه زیرلایه، آماده سازی لبه، هندسه و پارامترهای برش تعامل دارد. یک پوشش مناسب نمی تواند هندسه نامناسب، پارامترهای نادرست، یا تخلیه ناکافی تراشه را به طور کامل جبران کند و باید در کنار این عوامل ارزیابی شود نه به صورت مجزا. به جای یک توصیه عمومی، راهنمایی ویژه مواد را درخواست کنید خانواده های پوشش در بین تامین کنندگان و فرمولاسیون های خاص رفتار متفاوتی دارند. هنگام درخواست توصیه پوشش، مواد و درجه دقیق قطعه کار، نوع عملیات، ابزار فعلی و پوشش در صورت وجود، پارامترهای برش و علائم خرابی خاص مشاهده شده را ارائه دهید تا تامین کننده بتواند یک پوشش را با مکانیسم واقعی به جای دسته بندی مواد عمومی مطابقت دهد. اعتبار سنجی در دستگاه واقعی و راه اندازی ادعاهای عملکرد پوشش از ادبیات عمومی یک مرجع شروع هستند. سود واقعی به استحکام خاص دستگاه، استراتژی خنک کننده، پارامترهای برش و وضعیت قطعه کار بستگی دارد و باید قبل از اینکه به عنوان یک فرآیند ثابت به کار گرفته شود، از طریق آزمایشات کنترل شده روی ماشین تأیید شود. اشتباهات رایج در انتخاب پوشش با فرض اینکه پوشش گرانتر همیشه بهتر است یک پوشش ممتاز که برای حالت خرابی اشتباه انتخاب شده است، از یک پوشش مناسب و کم‌هزینه بهتر عمل نمی‌کند. پوشش را با مکانیسم شکست غالب تطبیق دهید، نه تنها با سطح قیمت. در نظر گرفتن "نانو" به عنوان یک تضمین عملکرد متمایز همانطور که در بالا بحث شد، "نانو" یک رویکرد ساختاری را توصیف می کند، نه یک شیمی ثابت یا بهبود ویژگی تضمین شده. بپرسید که نانوساختار چه خانواده پوشش پایه و مزایای خاصی را در نظر گرفته است. نادیده گرفتن تعاملات زیرلایه و هندسه یک پوشش نمی تواند جایگزین درجه، آماده سازی لبه یا هندسه نامناسب کاربید شود. اگر بعد از تغییر پوشش، ابزاری همچنان خراب می‌شود، به جای اینکه فرض کنید که پوشش به تنهایی مسئول است، زیرلایه، آماده‌سازی لبه و هندسه را بررسی کنید. کپی کردن انتخاب پوشش از یک ماده یا عملیات نامرتبط پوششی که در عملیات تکمیل آلومینیوم یک مغازه به خوبی عمل می کند، ممکن است مستقیماً به عملیات زبری فولاد ضد زنگ مغازه دیگر منتقل نشود، حتی اگر هر دو به طور کلی به عنوان "مواد دشوار" توصیف شوند. مناسب بودن پوشش را برای مواد و عملیات خاص تأیید کنید. رد شدن از اعتبارسنجی کنترل شده تغییر به یک پوشش جدید بدون مقایسه کنترل شده با ابزار قبلی، تأیید اینکه آیا پوشش یا تغییر همزمان دیگری مسئول هر گونه بهبود مشاهده شده یا رگرسیون بوده است، دشوار می کند. سوالات متداول آیا پوشش DLC برای ماشینکاری فولاد سخت شده مناسب است؟ DLC در درجه اول برای مقاومت در برابر اصطکاک و چسبندگی کم ارزش دارد که بیشتر مربوط به آلومینیوم و سایر مواد مستعد چسبندگی است. برای فولاد سخت شده، که در آن مقاومت حرارتی و اکسیداسیون معمولاً مهم‌تر است، یک پوشش PVD از خانواده TiAlN معمولاً با این کاربرد مرتبط است. توصیه خاص را با تامین کننده ابزار خود تأیید کنید. در واقع "پوشش نانو" به چه معناست؟ به طور کلی به پوششی با ویژگی‌های ساختاری در مقیاس نانو - مانند نانولایه یا ساختار دانه‌ای نانوکامپوزیت - اشاره دارد که در یک خانواده پوشش‌های موجود مانند PVD اعمال می‌شود، نه یک شیمی پوشش جداگانه. از تامین کننده بپرسید که نانوساختار در نظر گرفته شده کدام پایه شیمی و خاصیت خاصی را فراهم کند. آیا یک ابزار کاربید بدون پوشش می تواند از ابزار پوشش داده شده بهتر عمل کند؟ در برخی کاربردها، به‌ویژه پرداخت آلومینیوم یا پلاستیک‌ها و کامپوزیت‌های خاص، یک ابزار کاربید بدون پوشش و بسیار صیقلی می‌تواند به خوبی یا بهتر از یک ابزار روکش‌شده عمل کند، زیرا اولویت لبه تیز و کم اصطکاک است تا مقاومت حرارتی یا سایشی. این بستگی به مواد و عملکرد خاص دارد. چگونه بفهمم که پوشش من با برنامه من مطابقت ندارد؟ نشانه های عدم تطابق پوشش می تواند شامل عمر ابزار به طور غیرمنتظره برای درجه پوشش ذکر شده، لبه ساخته شده قابل مشاهده با وجود پوششی که برای مقاومت چسبندگی به بازار عرضه شده است، یا پوسته پوسته شدن زودرس پوشش تحت بارهای برش معمولی باشد. بررسی حالت شکست در برابر مکانیسم مورد نظر پوشش می تواند به شناسایی عدم تطابق کمک کند. هنگام درخواست توصیه پوشش چه اطلاعاتی را باید ارائه دهم؟ مواد و درجه قطعه کار خاص، نوع عملکرد، هندسه و پوشش فعلی ابزار، در صورت وجود، پارامترهای برش، روش خنک کننده، و توضیح یا عکسی از علائم خرابی خاص مشاهده شده (چسبندگی، تغییر رنگ حرارتی، سایش ساینده، یا پوسته پوسته شدن پوشش) را ارائه دهید. نتیجه گیری انتخاب پوشش باید از حالت شکست پیروی کند، نه عادت یا سطح قیمت به تنهایی. پوشش‌های PVD مانند TiAlN مقاومت حرارتی و اکسیداسیون مربوط به فولاد سخت شده و آلیاژهای با دمای بالا را نشان می‌دهند، پوشش‌های DLC به اصطکاک و چسبندگی مربوط به آلومینیوم و مواد مشابه می‌پردازند، و پوشش‌های «نانو» نشان‌دهنده اصلاح ساختاری است که می‌تواند در این خانواده‌ها به جای یک دسته جداگانه اعمال شود. تطبیق شیمی پوشش با مکانیزم شکست غالب، و اعتبار بخشیدن به انتخاب در دستگاه و راه اندازی واقعی، نتایج قابل اعتمادتری نسبت به پیش فرض برای پوشش آشنا بدون توجه به مواد ایجاد می کند. Supal (Changzhou) Precision Tools Co., Ltdابزار آسیاب کاربیدومته های کاربیدبا گزینه های پوشش مناسب برای مواد مختلف قطعه کار، از جمله محلول های مورد استفاده درماشینکاری فولاد ضد زنگ. برای درخواست توصیه پوشش،با سوپال تماس بگیریدبا مواد و درجه قطعه کار، نوع عملیات، ابزار و پارامترهای فعلی، و شرحی از علائم سایش یا خرابی خاص مشاهده شده. این اطلاعات به شناسایی ترکیب پوشش و بستر مناسب با کاربرد واقعی شما برای اعتبارسنجی روی ماشین کمک می کند.

2026

09/22